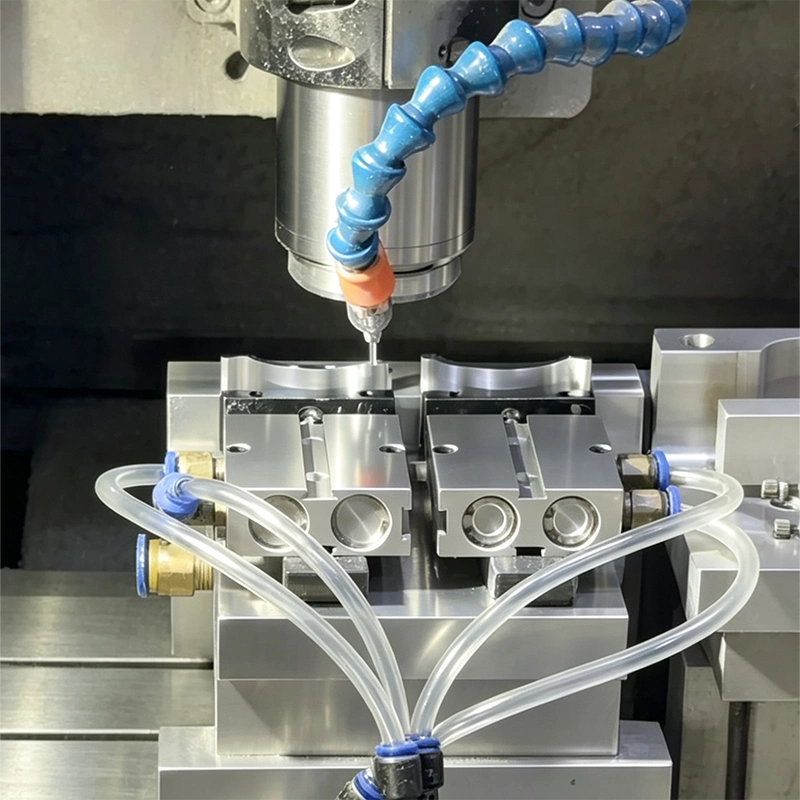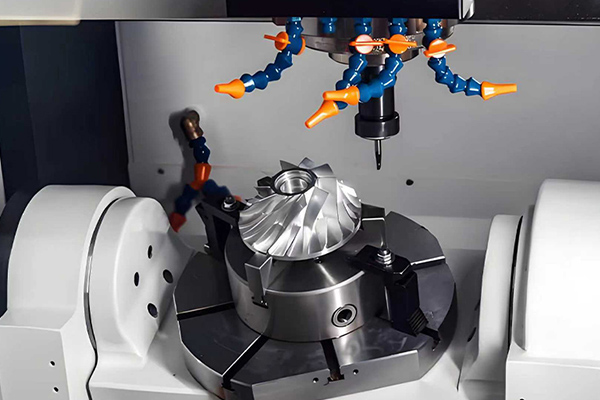
5 axis CNC machining is milling work in which the cutting tool can approach the part from almost any direction. A conventional three-axis mill moves the tool along X, Y and Z. Add two rotary axes — usually a trunnion table that tilts in B and rotates in C, or a tilting spindle head — and the cutter can be presented to the surface at an angle. Those two extra axes are what turn three linear movements into genuine five axis machining, and what separates a five axis CNC machine from a fast three-axis mill fitted with a rotary indexer.
5 轴 CNC 加工(5 axis CNC machining)指刀具可以从几乎任意方向接近零件的铣削加工。普通三轴铣床只沿 X、Y、Z 三个直线轴移动刀具;再加上两个旋转轴——通常是 B 向倾斜、C 向回转的摇篮工作台,或可摆动的主轴头——刀具就能以倾斜角度贴合工件表面。正是这两个附加轴,把三个直线运动变成了真正的五轴加工,也让五轴 CNC 机床区别于「加装回转分度盘的高速三轴铣床」。
A five axis cnc machining center is not simply a three-axis machine with two motors bolted on. The control has to interpolate all five drives simultaneously while compensating for tool length, and that compensation — usually called tool centre point control, or TCPC — is what keeps the tool tip on the programmed path while the head tilts. This is the axis of CNC machine capability most buyers underestimate: without a controller that does this well, a five axis cnc milling machine can only cut accurately in indexed 3+2 positions, and every genuinely simultaneous pass has to be programmed around the machine's exact kinematics. Ask about TCPC before comparing quotes, because two machines that look identical on the spec sheet can behave very differently on a contoured surface.
五轴 CNC 加工中心不等于「三轴机床外挂两个电机」。数控系统必须同时插补五个轴,并实时补偿刀具长度——这一补偿通常称为刀尖点控制(TCPC),正是它让刀具在主轴头倾斜时刀尖仍然走在编程轨迹上。这是买家最容易低估的一层能力:没有这一功能的五轴 CNC 铣床,只能在 3+2 定位状态下保证精度,每一次真正的联动加工都得针对该机床的具体运动学单独编程。比价之前请先问清 TCPC,因为参数表上看起来完全一样的两台机床,加工曲面时的表现可能天差地别。
There are two ways to run it, and the difference drives both capability and price. Positional work, widely called 3+2, indexes the rotary axes to a fixed angle and then cuts with three axes. Simultaneous five axis machining moves all five at once, keeping the tool in continuous contact with a curved surface. The first is a cheap way to reach a hole on an angled face; the second is how impellers, impeller-bladed pump bodies and contoured heat sinks get finished in one continuous pass. Knowing which one your part actually needs is the single largest cost lever.
实际操作有两种方式,能力与价格差别很大。定位加工(业内常称 3+2)把旋转轴转到固定角度后按三轴方式切削;联动五轴加工则五个轴同时运动,刀具与曲面保持连续接触。前者是加工斜面上孔位的低成本做法,后者才是叶轮、叶片泵体和带曲面散热结构能够在一次连续走刀中成型的原因。搞清楚零件真正需要哪一种,是最大的成本控制杠杆。
The strongest argument for a five axis CNC machine is not speed, it is accuracy. Every unclamp-and-refixture cycle introduces a small datum shift, and those shifts stack. A bracket that needs five faces worked may take five setups on a three-axis mill, each one adding its own locating error. Machine the same part in one fixturing on five axes and that stack-up disappears, which is why complex parts often come off a five axis CNC machine more accurate even when the individual cuts are no faster.
选用五轴 CNC 机床最有力的理由不是速度,而是精度。每一次拆下重新装夹都会带来微小的基准偏移,而这些偏移会累积。一个需要加工五个面的支架,在三轴铣床上可能要装夹五次,每次都叠加自己的定位误差。同样的零件在五轴上一次装夹完成,这种累积误差就消失了——这正是复杂零件在五轴上做出来的精度往往更高的原因,即使单刀切削速度并不更快。
On tolerance, treat ±0.01 mm as a capability, not a default. We hold ±0.01 mm routinely on features whose datum structure supports it, and looser everywhere else, because holding a tight number on a face that nothing locates against costs money and buys nothing. Tell us which dimensions actually control assembly and we will build the process plan around them; everything else gets a sensible general tolerance.
关于公差,请把 ±0.01mm 当作能力上限而不是默认值。对基准结构能够支撑的特征,我们常规可稳定做到 ±0.01mm;其余位置放宽处理——在一个没有任何配合关系的面上守住极严公差只会增加成本而没有实际意义。请告诉我们哪些尺寸真正控制装配,我们会围绕它们编制工艺,其余按合理的通用公差执行。
5 axis machining costs more per machine hour than three-axis work, and the reasons are structural: the machine itself costs several times as much, CAM programming takes longer, tool paths need collision simulation, and every setup needs verification. It also saves money in places buyers rarely see — fewer fixtures to build, fewer inspections, fewer scrapped parts from handling damage, and fewer days in the schedule. As a working rule, once a part needs three or more setups on a three-axis machine, or has features a straight tool simply cannot reach, five axis machining is usually the cheaper route overall.
五轴加工的机床小时费率高于三轴,原因是结构性的:设备本身的购置成本高出数倍,CAM 编程耗时更长,刀路需要碰撞模拟,每个装夹方案都要验证。但它也在采购方不易察觉的地方省钱——更少的夹具、更少的过程检验、更少的搬运报废,以及更短的交期。经验法则是:当一个零件在三轴机床上需要三次以上装夹,或存在直柄刀具根本无法触及的特征时,五轴加工在总成本上通常反而更便宜。
Materials behave differently once the tool stays engaged longer. On a five axis CNC machine we regularly run 6061-T6 and 7075-T6 aluminium, 304 and 316 stainless, Ti-6Al-4V titanium, C360 brass and engineering plastics such as PEEK. Titanium in particular rewards shorter tools: Ti-6Al-4V yields around 880 MPa at a density of 4.43 g/cm³, so it resists cutting and holds heat in the cut zone, and tilting the tool lets us use a stub-length cutter that a straight approach could never fit.
刀具持续参与切削的时间变长后,材料的表现也不同。在五轴 CNC 机床上,我们常规加工 6061-T6 与 7075-T6 铝合金、304 与 316 不锈钢、Ti-6Al-4V 钛合金、C360 黄铜以及 PEEK 等工程塑料。钛合金尤其受益于短刀具:Ti-6Al-4V 的屈服强度约 880MPa、密度 4.43g/cm³,既难切削又把热量留在切削区,而刀具倾斜后可以使用直进方式根本装不下的短刃铣刀。
Our heaviest five axis CNC machining volume is audio equipment — amplifier heat sinks with contoured fin fields, microphone bodies and yokes, speaker baskets and driver plates, and rack-mount front panels with angled port reliefs. A CD-textured face that would need three fixtures on three axes comes off one five axis setup with the datums intact, and the cosmetic surfaces match across the batch because no datum was re-established mid-process. Aerospace brackets, medical instrument bodies, optical mounts and UAV structural parts follow the same logic.
我们最大的五轴 CNC 加工业务量来自音频设备——带曲面散热齿阵的功放散热器、麦克风壳体与支架、扬声器盆架与单元安装板,以及带有斜面端口避让的机架式前面板。一个在三轴上需要三套夹具的 CD 纹面,在五轴上一次装夹即可完成并保持基准统一;整批外观面的一致性也因此更好,因为过程中从未重新建立基准。航空航天支架、医疗器械壳体、光学座体与无人机结构件遵循同样的逻辑。
Send us the model and we will tell you which features genuinely need five axis machining, which do not, and what the honest lead time is — usually a DFM review and quotation back within 24 hours. See also our 5-axis CNC machining guide for parameter detail, or CNC milling for simpler prismatic work.
把 3D 模型发给我们,我们会明确告知哪些特征真正需要五轴加工、哪些不需要,以及真实的交期——通常在 24 小时内回复 DFM 评审与报价。参数细节可参考我们的 五轴 CNC 加工指南;较简单的棱柱类零件可查看 CNC 铣削。