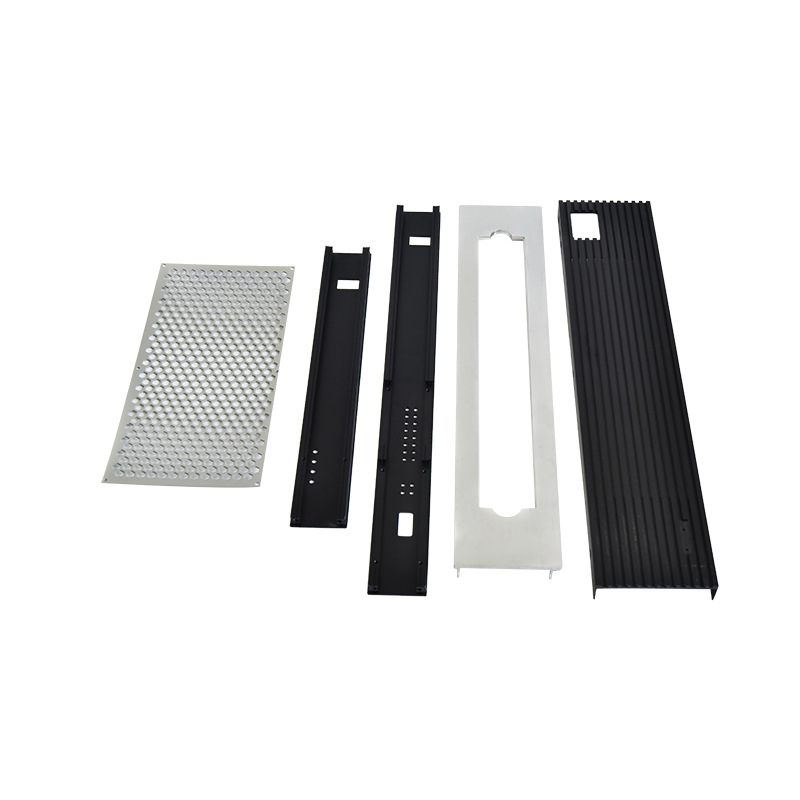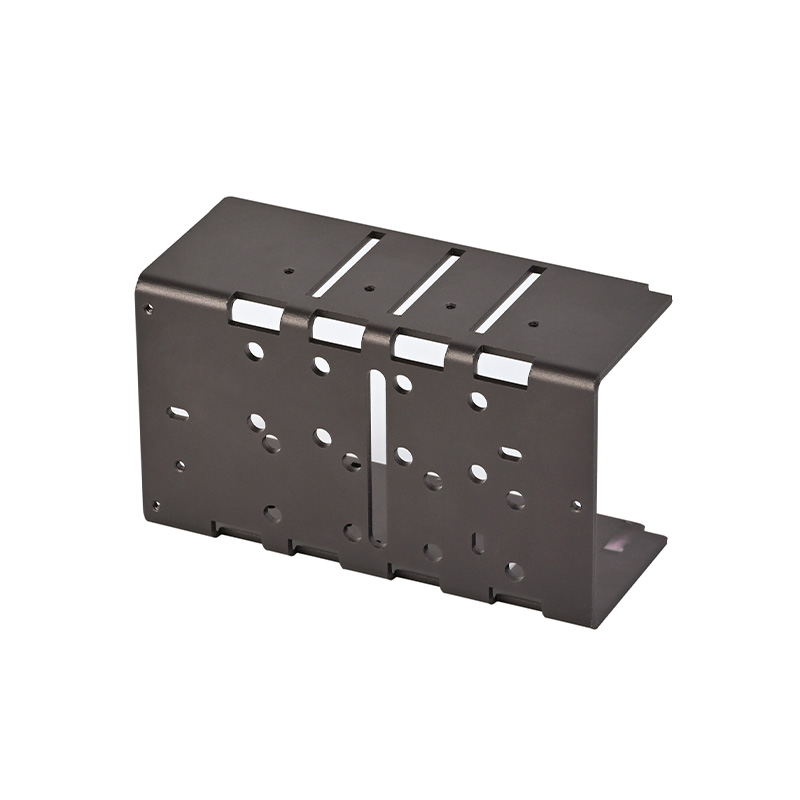
CNC sheet metal fabrication builds a three-dimensional part from a flat blank by cutting, bending and joining, instead of removing material from solid stock the way CNC machining does. The flat pattern is unfolded in CAD with a bend allowance calculated for the specific material, thickness and inside bend radius, then the blank is cut on a fibre laser or turret punch. Every bend after that runs on a CNC press brake with a programmed back-gauge, so the same program delivers the same part on the tenth run and the ten-thousandth.
CNC 钣金加工是从一块平板出发,经切割、折弯与连接做出立体零件,而不是像 CNC 加工那样从实心料上削除材料。展开图在 CAD 里按材料、板厚与内折弯半径计算折弯补偿后展开,再用光纤激光或转塔冲切出毛坯。之后每道折弯都在带程序后挡料的 CNC 折弯机上完成,因此同一个程序第十次和第一万次做出来的零件是一致的。
Tolerances follow the process, not the machine. A laser-cut profile holds about ±0.1 mm as standard and ±0.05 mm on critical cut-outs, while bend-to-bend dimensions accumulate roughly ±0.2 mm per bend unless the design controls it with locating features or a welded fixture. When an assembly genuinely needs ±0.01 mm on a bore, a thread or a flat sealing face, that feature is normally machined after the sheet metal work is finished — a hybrid route we run in one facility. Our guide to CNC machining vs sheet metal fabrication sets out the decision rules feature by feature.
公差跟着工艺走,而不是跟着机床走。激光切割轮廓标准约 ±0.1 mm,关键开孔 ±0.05 mm;折弯到折弯的尺寸则每道折弯累积约 ±0.2 mm,除非设计用定位特征或焊接夹具把它控制住。当装配真的需要孔、螺纹或密封面达到 ±0.01 mm 时,这个特征通常在钣金完成后再来加工——这道混合工艺我们在同一个厂区里就能走完。CNC 加工 vs 钣金加工指南按特征逐条给出了选择规则。
Lead time is the strongest argument for sheet metal. With no tooling to build, a laser-cut and bent prototype enclosure ships in 3 to 7 working days from a released drawing, and production repeats run 7 to 15 days including powder coating. For flat parts with simple geometry and high annual volume, progressive die stamping eventually undercuts the laser on unit price; depending on part size the crossover usually sits somewhere between a few thousand and tens of thousands of pieces.
交期是钣金最有力的理由。不需要开模,图纸确认后激光切割折弯的样机外壳 3 到 7 个工作日就能出货,量产的重复订单含粉末喷涂 7 到 15 天。对于几何简单、年用量大的平板件,连续模冲压最终会在单价上低于激光切割;按零件大小不同,这个交叉点通常在几千件到几万件之间。
Four design moves cut cost further than any negotiation: keep hole diameters at or above material thickness, use one uniform bend radius across the whole part, keep holes at least 1.5 times material thickness away from any bend line, and standardise on a single sheet thickness per assembly. Each one removes a set-up, a tool change or a rework loop. Send a STEP file for a free DFM review and a firm quote within 24 hours.
有四个设计动作比任何议价都更能降本:孔径不小于板厚、全零件用统一的折弯半径、孔位离折弯线至少 1.5 倍板厚、每个装配统一用一种板厚。每一项都能省掉一次装夹、一次换刀或一次返工循环。发 STEP 文件过来,含免费 DFM 评审,24 小时内出正式报价。