
An RFQ came in last spring with 214 dimensions on the drawing and one line in the quality notes: "Cpk 1.67 on all characteristics, PPAP Level 3". We priced it two ways. Full capability study on every dimension: 214 measurements per part, 32 parts, a second operator to check them, roughly $9,400 and three weeks of inspection labor before a single part shipped. Then we asked the obvious question, which nobody had asked: which of these 214 dimensions actually keeps the part from working?
Nine did. Four bore diameters, two face-to-face lengths, three thread positions. We wrote a control plan around those nine, ran the study on those nine, and quoted the remaining dimensions to the drawing tolerances under our standard inspection plan. The cost came down to about $2,800 and the launch happened on time. Six months later the customer told us the original line had been copied from a template their previous supplier had sent them.
*(Composite example; details changed.)*
That is the point of a control plan and a capability study. They are not paperwork you bolt on at the end of a project. They are the two documents that decide where your money goes, and on most programmes the expensive mistake is not a bad process. It is applying the same requirement to everything.
What a control plan is, and what it is not
A control plan is a written description of how a specific part is going to be controlled through a specific process, at a specific facility. Not a quality manual, not a work instruction, not an inspection checklist you download and fill in. It lists, operation by operation, what is measured, how often, with what, and what happens when the number moves.
It is a living document with three phases, and the phase matters because the content changes:
| Phase | When it applies | What it controls | Typical sample plan |
|---|---|---|---|
| Prototype | First parts, process not yet fixed | Dimensional conformance, material, and the unknowns | 100% on critical features, reduced sampling on the rest |
| Pre-launch | Process fixed, volume ramping | Added process parameters, gauge studies, capability | Frequent sampling plus SPC start-up |
| Production | Steady state | Product and process characteristics, reaction plans | SPC, periodic audits, defined frequency |
Most arguments we get asked to settle come from a production control plan being used during prototype, or a prototype control plan still running eighteen months into production. Same document, wrong phase, and suddenly every deviation is a crisis.
The columns that carry the weight
A control plan template, described alongside the process flow in our services overview, has a dozen or more columns. Four of them decide whether the document does anything.
- Special characteristic class. The features that matter, with the customer's symbol where they use one. This is the column that turned 214 into nine.
- Evaluation and measurement technique. The actual gauge, and the resolution. "Caliper" and "0.001 mm indicator on a granite stand" are not the same control, and only one of them can see a 0.03 mm band.
- Sample size and frequency. Tied to the phase, tied to the risk, and honestly costed.
- Reaction plan. What the operator does at 3 in the morning when the number drifts: contain, tag, notify, adjust, or stop. A control plan without a reaction plan is a report, not a control.
Capability indices: four numbers, four different questions
| Index | Formula | The question it answers |
|---|---|---|
| Cp | (USL - LSL) / (6 x sigma within) | Is the spread narrow enough to fit the band? |
| Cpk | min[(USL - mean), (mean - LSL)] / (3 x sigma within) | Is it narrow enough and centred? |
| Pp | (USL - LSL) / (6 x sigma overall) | Same as Cp, but over the whole run including drift |
| Ppk | min[(USL - mean), (mean - LSL)] / (3 x sigma overall) | Same as Cpk, but over the whole run including drift |
The within/overall split is the whole trick. Sigma within comes from variation inside a subgroup, which is a short window where nothing drifts. Sigma overall is computed across every part in the study. In a process with tool wear, thermal growth or material lot changes, the second number is bigger, and the gap between them is the drift.
Worked example: a Ø12 shaft with a 0.06 mm band
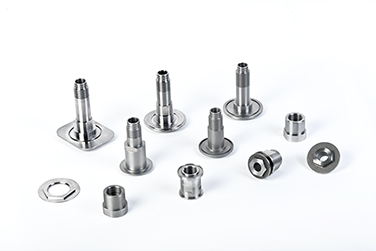
A turned shaft, Ø12.000 ±0.030, produced on our CNC turning service. LSL 11.970, USL 12.030, band 0.060 mm. We ran 32 pieces in eight subgroups of four. Mean 12.005, sigma within 0.006, sigma overall 0.010.
| Index | Calculation | Result |
|---|---|---|
| Cp | 0.060 / (6 x 0.006) | 1.67 |
| Cpk | min[(12.030 - 12.005), (12.005 - 11.970)] / (3 x 0.006) = min[0.025, 0.035] / 0.018 | 1.39 |
| Pp | 0.060 / (6 x 0.010) | 1.00 |
| Ppk | min[0.025, 0.035] / (3 x 0.010) = min[0.025, 0.035] / 0.030 | 0.83 |
Read those four numbers in order and the process tells you what is wrong with it.
Cp is 1.67 but Cpk is 1.39. The spread fits the band with room to spare, but the mean sits at 12.005 instead of 12.000. That 0.005 mm mean shift accounts for the whole 0.28 gap between Cp and Cpk, and recovering it costs nothing: reset the tool offset and Cpk becomes Cp. A machine purchase would not have fixed it, and neither would a better bar of steel.
Ppk is 0.83 against a Cpk of 1.39. That gap is drift. Using the usual additive variance model, the between-subgroup component works out at roughly sqrt(0.010² - 0.006²) = 0.008 mm. Before anyone buys anything, plot the subgroup means in production order. Tool wear is the most likely explanation and a shorter tool change interval or wear offset compensation usually removes it, but thermal growth, a material lot change and an operator shift all produce the same statistical pattern.
How many pieces, and why 32 is not enough for a big claim
Our default initial study is 25 subgroups of five, so 125 pieces, drawn over a period long enough to include at least one tool change, one material lot and one operator shift. Customer-specific requirements name their own designs and we follow those when they exist. That is what makes sigma overall meaningful.
Many programmes accept 32 pieces for a pre-launch study, and we will run it if that is what the customer requires. What we will not do is pretend the number is precise. At n = 32 the confidence interval on the index is wide, of the order of a quarter of its value, so a study reporting Cpk 1.39 is honestly telling you the process sits somewhere near 1.05 to 1.75 depending on how the bounds are computed. A supplier quoting "Cpk 1.67" off 32 pieces is quoting the middle of a range whose bottom end fails. If the characteristic is safety related, buy the 125 pieces.
Two more conditions people skip. Capability indices assume the process is in statistical control: run the control chart first, because indices computed on an unstable process are arithmetic, not information. And they assume normality. A bimodal distribution from two cavities or two machines will produce a plausible-looking Cpk that describes neither.
On one-sided characteristics, such as flatness 0.05 max, there is no Cp at all. Only Cpk applies, and it only has the upper term.
What buyers actually ask us
Our customer demands Cpk 1.67 on everything. Can you do it? We can measure it, and we will tell you what it costs before you commit. The more useful move is to identify the characteristics where 1.67 protects something, hold those, and let the rest run at standard inspection. We make that call during the free DFM review, which is also where we catch the datum problems described in the GD&T true position guide.
Why did you ask for 125 pieces when our requirement calls for 32? Because we will run the 32 if that is what your customer-specific requirement names, label the result preliminary, and put its confidence interval next to it rather than pretending the point estimate is exact. On IATF 16949 programmes the customer usually agrees once they see the interval.
Do you run control plans on non-automotive work? Yes, in a lighter form. A 500-piece run of audio faceplates does not need a full PPAP document set, but whoever runs it still needs a written list of which dimensions get checked and how often. The discipline scales even when the paperwork does not, and the low volume guide shows what we keep when the run is 300 pieces instead of 300,000. Our medical device work sits between the two.
What if the study fails? Then the process is telling you something, and the most common answer is that the tolerance band and the process capability were never matched. We would rather change the process or discuss the tolerance band than massage the analysis until the failure disappears.
The study belongs in the first article inspection package, and the measurement method behind every number is the one described in our CNC inspection methods guide. Whether that measurement can be trusted at all is a separate question, and it is answered by a gage R&R study.
Frequently asked questions
What is the difference between a control plan and an inspection plan?
An inspection plan lists what gets checked. A control plan also records the process parameters, the sampling frequency, the control method and the reaction plan, operation by operation, and it names the special characteristics. An inspection plan can be written for one part; a control plan describes a part running through a specific process at a specific facility.
What Cpk value should I require from a supplier?
The AIAG APQP and PPAP manuals ask for a Ppk above 1.67 on a new process at launch and a Cpk of at least 1.33 once the process is stable and running, and plenty of customers write stricter numbers on top of that. Ask for Cpk and Ppk computed from the same time-ordered run and read them together: Ppk carries the drift that Cpk hides, which is why a 1.33 Ppk can be a harder requirement to meet than a 1.67 Cpk figure quoted on its own.
Why is Ppk lower than Cpk on my report?
Because the process drifted during the study. Cpk uses variation within a short subgroup, Ppk uses variation across the whole run. The gap is tool wear, thermal growth or a material lot change, and it is the most useful diagnostic on the page.
Can you do a capability study on a 50 piece prototype?
We can compute the indices, and we will label them as preliminary. At 50 pieces the numbers describe that batch, not the process, and no launch decision should rest on them. If the programme needs a real capability number, plan 125 pieces across at least one tool change.
Conclusion
A control plan and a capability study exist to answer one question: where does the risk actually sit? On most drawings it sits in under ten dimensions, and across our 200+ CNC machines finding them is worth more than any amount of inspecting. We write the control plan, run the study, and hand over both documents with the parts, alongside the CNC machining tolerance decisions that set the bands in the first place, because you cannot audit a number you cannot reproduce.
In 23+ years we have learned that a ±0.01 mm claim only survives a customer's incoming inspection when the gauge, the sample frequency and the stop rule are written down first. Send us the drawing, the volume and any customer-specific quality requirements. We will tell you which characteristics deserve a capability study, which ones do not, and exactly what the difference costs, and we run that work under IATF 16949, ISO 9001 and ISO 13485. DFM is free and a quote comes back within 24 hours. Talk to our team.